
Animal Feed Production Line: Complete Guide
Every ton of feed begins as a formula-and ends as a promise of livestock performance. Feed mills convert raw grains, protein meals, and additives into consistent rations through precisely engineered production lines. This guide examines each stage: intake and storage, grinding, batching and mixing, pelleting and extrusion, plus the quality control, automation, packaging, and safety systems that keep modern operations efficient and compliant.
Overview of Animal Feed Production Lines
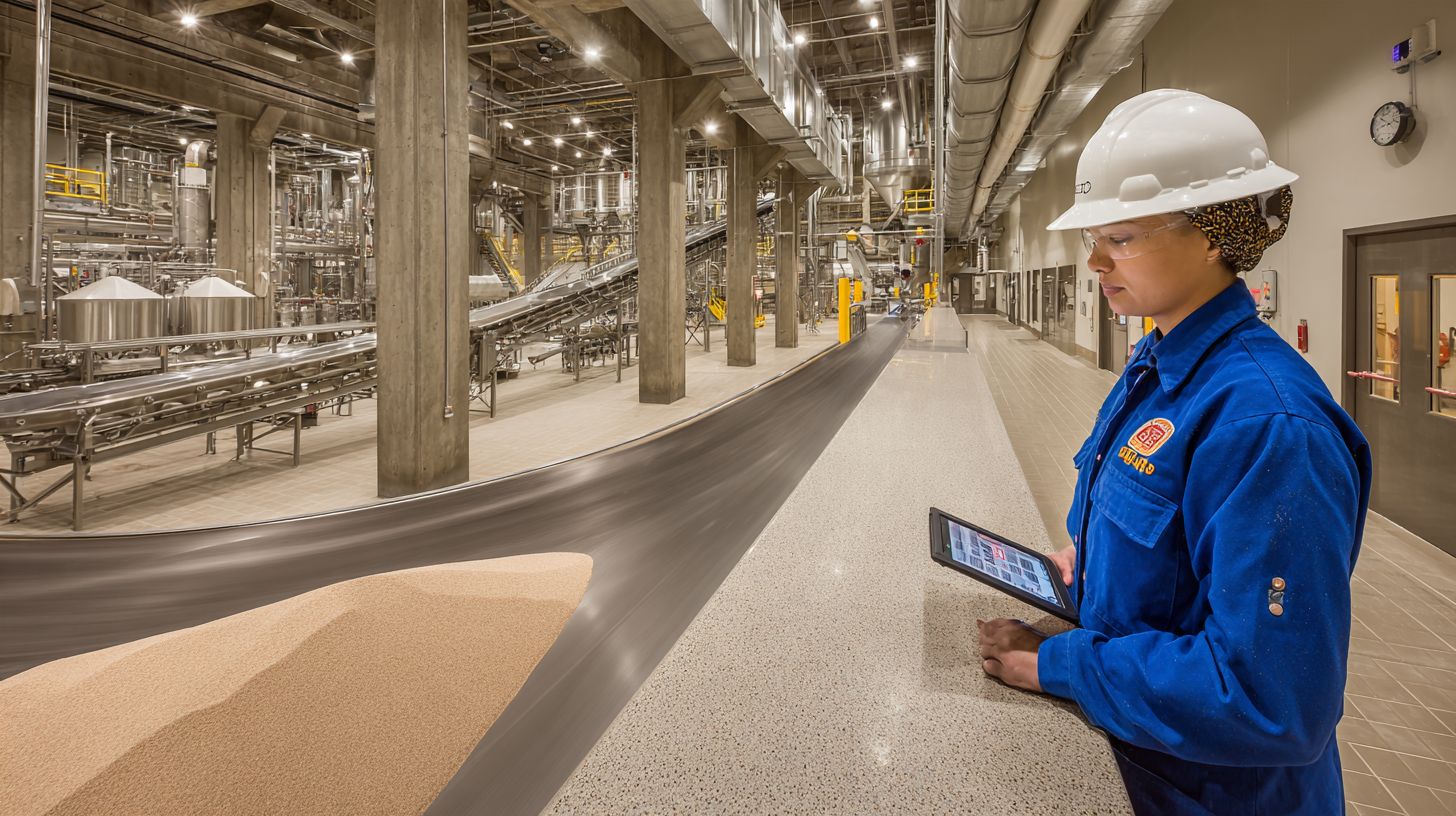
A modern animal feed production line can process 5-50 tonnes per hour, transforming raw grains and protein meals into nutritionally balanced compound feed through a sequence of grinding, batching, mixing, pelleting or extrusion, drying, cooling, and packaging stages.
Small farm-scale lines often run at the lower end of this range, while large commercial feed manufacturing plants operate at higher throughput capacity with fully automated PLC control. The finished product may be mash feed, pelleted feed, extruded feed, or crumbled feed, depending on the target species and its nutritional requirements.
A well-designed process flow diagram maps every step from raw material intake to the bagging machine, helping engineers plan equipment selection, conveyor system routing, and storage silo placement before construction begins.
Types of Feed (Poultry, Livestock, Aqua)
Poultry feed typically contains 18-22% protein and is often crumbled for chicks, while aquaculture feed requires 28-45% protein and is extruded for water stability.
| Feed Type | Protein Range | Common Ingredients | Processing Method | Special Considerations |
|---|---|---|---|---|
| Poultry (broiler) | 20-24% | Corn, soybean meal, vitamins, amino acids | Grinding, mixing, pelleting, crumbling | Pellet durability index affects feed conversion ratio |
| Poultry (layer) | 16-18% | Corn, soybean meal, calcium, minerals | Grinding, mixing, pelleting | Higher calcium for shell strength |
| Swine (starter, grower, finisher) | 14-22% | Corn, soybean meal, wheat, minerals, enzymes | Grinding, batching, mixing, pelleting | Particle size and mixing uniformity are critical |
| Aqua (shrimp, tilapia, salmon) | 28-45% | Fishmeal, soybean meal, binders, probiotics | Extrusion, drying, cooling | Floating pellets need water stability |
| Ruminant (dairy, beef) | 12-18% | Barley, oats, molasses, meat and bone meal | Grinding, mixing, sometimes pelleting | Molasses addition improves palatability |
Nutritional requirements dictate the processing route. Aqua feed relies on an extruder to produce floating or sinking pellets with high water stability, while ruminant feed may incorporate molasses and bypass protein for rumen health.
Ingredient selection follows species needs closely. Poultry rations lean on soybean meal for digestible protein, whereas aqua formulations depend on fishmeal and specialized binders to hold pellets together underwater.
Key Stages of Production
The production line typically involves eight core stages: raw material intake, grinding, batching, mixing, pelleting or extrusion, drying, cooling, and packaging, with each stage critical to final feed quality.
- Raw material intake and storage: Corn, wheat, barley, and protein meals arrive by truck and are stored in silos or flat warehouses. A hammer mill or roller mill then reduces particle size to the target range.
- Grinding process: The hammer mill breaks grain into uniform particles using rotating hammers and screens. Particle size directly influences mixing uniformity and pellet quality.
- Batching and mixing: A weighing scale and dosing system measure each ingredient according to feed formulation, then a feed mixer blends them with premix, vitamins, minerals, and additives.
- Pelleting or extrusion: A feed pellet mill forces conditioned mash through dies and rollers to form dense pellets, while an extruder cooks and shapes aqua feed under high pressure and moisture.
- Drying and cooling: A dryer removes excess moisture, and a cooler brings pellets down to safe storage temperature. Moisture content must stay within specification to prevent mold.
- Crumbling and screening: A crumbler breaks pellets into smaller pieces for young animals. Sieving removes fines, which are recycled back into the process.
- Packaging: A bagging machine fills, weighs, and seals bags, while a palletizer stacks them for dispatch. A conveyor system and bucket elevator link each stage.
- Automation and quality control: PLC control monitors throughput, energy consumption, and traceability. Magnets, metal detectors, and HACCP checks protect feed safety.
A simple process flow diagram shows raw materials entering the hammer mill, moving through ingredient batching and the feed mixer, then to the pelletizer or extruder, followed by the dryer, cooler, crumbler, and finally the packaging line.
Not every feed manufacturing plant includes pelleting. Mash feed lines skip the pellet mill and extruder entirely, moving ground and mixed material straight to bagging, which lowers energy consumption and wear on dies and rollers.
Raw Material Intake and Storage
A typical feed mill stores 500-5,000 tonnes of raw materials in silos and flat warehouses, receiving grains like corn and wheat by truck or rail and protein meals in bags or bulk. Proper intake procedures protect every downstream stage of the animal feed production line.
Incoming loads are weighed, sampled, and inspected before unloading. Rejecting contaminated or out-of-spec batches at this point prevents costly problems in the hammer mill, feed mixer, and pellet mill later on.
Storage capacity should match throughput capacity and delivery cycles. A feed manufacturing plant that runs continuously needs enough buffer stock to keep the grinding process and mixing process running without interruption.
Grains, Protein Meals, and Additives
Corn and wheat provide energy, soybean meal and fishmeal supply protein, while premixes of vitamins, minerals, and amino acids are added at 0.1-1% inclusion rates to meet nutritional requirements. Each category demands its own handling and storage approach.
| Category | Examples | Typical Inclusion Rate | Key Function |
|---|---|---|---|
| Energy Sources | Corn, wheat, barley, oats | 50-70% | Supply carbohydrates and energy for growth and maintenance |
| Protein Sources | Soybean meal, fishmeal, meat and bone meal | 15-35% | Provide amino acids for muscle development and milk production |
| Additives | Vitamins, minerals, amino acids, enzymes, probiotics | 0.1-1% | Correct nutrient gaps and support digestion and health |
| Other | Molasses, fats, binders | 1-5% | Improve palatability, energy density, and pellet binding |
Quality checks focus on moisture content, protein content, and mycotoxin testing. Grain received above safe moisture levels should be dried before storage to prevent mold growth and spoilage.
Storage conditions matter just as much as the checks themselves. Silos and warehouses should stay dry, ventilated, and pest-free, with stock rotated on a first-in, first-out basis so older material moves through the feed production line first.
Silos, Bins, and Handling Systems
Storage silos range from 50 to 1,000 tonnes and are equipped with screw conveyors, bucket elevators, and rotary valves to transport materials to the batching system without cross-contamination. Vertical silos suit free-flowing grains, while flat-bottom bins handle meals that tend to bridge or cake.
Liquid tanks hold molasses and fats, often fitted with heating coils to keep viscosity low enough for accurate dosing. Each vessel connects to the weighing scale and dosing system through dedicated lines.
Handling equipment follows material characteristics. Bucket elevators move bulk vertically, screw conveyors shift it horizontally, and pneumatic systems carry powders and fine premixes. A well-designed conveyor system keeps ingredient batching accurate and repeatable.
Dust control protects both workers and equipment. Aspiration systems pull dust from transfer points, cyclone separators drop coarse particles, bag filters capture fines, and airlocks discharge collected material without losing pressure.
Clean-out procedures between batches prevent cross-contamination, especially when switching between medicated and non-medicated formulas. Magnets and metal detectors placed before the feed mixer catch tramp metal that could damage hammers, screens, dies, and rollers.
A simple process flow diagram helps operators visualize the route: intake pit, bucket elevator, storage silo, screw conveyor, weighing scale, feed mixer, then onward to the pellet mill or extruder. Clear labeling of lines and valves reduces human error during changeovers.
Grinding and Particle Size Reduction
Grinding reduces raw materials to a particle size of 0.5-2 mm, which is critical for proper mixing and pellet quality, using either hammer mills or roller mills depending on the ingredient. This step in an animal feed production line increases the surface area of grains such as corn, wheat, and barley so digestive enzymes and the feed mixer can work more effectively.
Smaller, more consistent particles improve mixing uniformity, which keeps vitamins, minerals, and additives evenly distributed throughout the batch. Uniform size also supports stable pellet durability when the mash reaches the feed pellet mill.
Target particle size varies by species and feed type. Poultry feed and swine feed often call for finer grinds, while ruminant feed and mash feed tolerate coarser particles. Aquaculture feed and extruded feed typically require the finest reduction before extrusion.
Grinding also affects downstream equipment. Oversized particles strain the pelletizer and dryer, while overly fine dust increases load on the aspiration system and bag filter. Matching grind size to the formulation protects the whole process.
Hammer Mills and Roller Mills
Hammer mills use swinging hammers to impact and shatter grains, achieving particle sizes of 0.5-2 mm with capacities up to 50 t/h, while roller mills crush grains between corrugated rolls for a more uniform particle size distribution. Both designs sit near the front of a feed manufacturing plant, right after ingredient batching and weighing.
| Aspect | Hammer Mill | Roller Mill |
|---|---|---|
| Principle | Impact from swinging hammers | Compression between corrugated rolls |
| Particle Size Range | 0.5-2 mm, wide spread | 0.5-1.5 mm, narrow spread |
| Capacity | Up to 50 t/h | Up to 30 t/h |
| Energy Consumption | Higher per ton | Lower per ton |
| Maintenance | Screen and hammer replacement | Roll re-corrugation |
| Best For | Fibrous materials, varied ingredients | Grains such as corn and wheat |
Choose a hammer mill when the line handles diverse raw materials, including fibrous ingredients and byproducts. It offers flexibility across feed formulations, though hammers and screens wear faster and demand more energy per ton.
Select a roller mill when grains dominate the recipe and uniform particle size matters most. It uses less energy and produces fewer fines, but rolls need periodic re-corrugation and the unit handles fibrous material poorly.
Wear parts drive long-term cost. Keep spare hammers, screens, and rolls in the spare parts inventory to avoid unplanned downtime. Typical pricing runs from $5,000 to $50,000 for a hammer mill and $10,000 to $100,000 for a roller mill, depending on capacity and automation features.
Batching and Mixing Systems
Batching systems weigh ingredients to +-0.1% accuracy using scale hoppers and dosing screws, ensuring each batch meets the precise nutritional profile defined by feed formulation software. This precision protects the feed conversion ratio and keeps every bag of livestock feed within specification.
Typical batch sizes in a feed manufacturing plant range from 500 to 2,000 kg, with mixing times of 2 to 5 minutes depending on the feed mixer design. Uniform blending of premix, vitamins, minerals, and amino acids depends on both weighing accuracy and mixer performance.
Poor control at this stage invites cross-contamination between medicated and non-medicated formulas, a serious feed safety risk. The subsections below cover weighing accuracy, mixer selection, and mixing uniformity testing in detail.
Weighing Accuracy and Homogeneity
Achieving a coefficient of variation (CV) below 5% in mixing requires precise weighing (+-0.1% for micro-ingredients) and a mixer design that prevents dead spots and segregation. Bulk scales handle major ingredients such as corn, wheat, barley, and soybean meal at +-0.5% accuracy, while micro-scales dose additives, premix, and enzymes at +-0.1%.
Dosing hardware must match the material. Screw feeders suit free-flowing grain and meals, vibratory feeders handle fragile or bridging ingredients, and liquid addition systems inject molasses, fats, and liquid antioxidants through spray nozzles or flow meters. Each path feeds the weighing scale under PLC control, which logs every ingredient drop for traceability.
Mixer choice shapes homogeneity. A horizontal ribbon mixer works well for mash feed, a paddle mixer handles heavier rations, a twin-shaft mixer delivers fast, high-shear blending, and a vertical mixer suits smaller operations with limited floor space. Research suggests the twin-shaft design reaches uniformity faster, which shortens cycle time in a busy feed mill.
Verify performance with uniformity testing. Collect around 10 samples per batch and assay the CV of a tracer such as salt or a marker additive. One poultry feed mill reduced CV from 10% to 3% by upgrading to a twin-shaft mixer and optimizing mixing time to 3 minutes.
Prevent cross-contamination through sequence batching, running flush material between formulas, and dedicating lines to medicated feed. Pair these steps with dust control, an aspiration system, and a magnet or metal detector before the batch moves to the next stage of the animal feed production line.
Pelleting and Extrusion
Pelleting and extrusion transform mixed feed into durable pellets or expanded extrudates, improving feed conversion ratio by 5-15% and reducing waste, with pelleting capacities up to 40 t/h and extrusion up to 20 t/h. These processes also boost digestibility, cut dust, and make handling easier across the animal feed production line.
In a feed manufacturing plant, the pelleting process relies on conditioners, a feed pellet mill, and a pelletizer, while extrusion uses an extruder to cook and expand feed. Both routes typically finish with a dryer and cooler to stabilize moisture before storage.
Choosing between them depends on species and nutritional requirements. Poultry feed and swine feed often favor pelleted feed, while aquaculture feed frequently needs extruded feed that sinks or floats as required.
The sections below cover conditioning, die selection, and cooling, the core steps that determine pellet quality and throughput.
Conditioning, Dies, and Coolers
Conditioning feed with steam at 80-90 degreesC for 30-60 seconds gelatinizes starches and improves pellet durability, while die selection (thickness, hole diameter) and cooling to within 5 degreesC of ambient temperature ensure a Pellet Durability Index (PDI) above 95%.
Steam addition raises both moisture and temperature, softening raw materials so the pelletizer can press them without cracking. Retention time in the conditioner matters: too short and starches stay ungelatinized, too long and feed becomes sticky. Operators should monitor steam quality, aiming for dry, saturated steam rather than wet steam that adds excess water.
Die specifications directly shape pellet quality and energy consumption. Common hole diameters range from 2-6 mm, die thickness from 20-60 mm, and compression ratio is chosen based on feed formulation. Higher compression ratios suit dense compound feed, while lower ratios help poultry feed and mash feed blends flow freely.
Coolers bring pellets down to safe moisture content, usually 10-12%. Counterflow, horizontal, and vertical coolers each suit different layouts and throughput capacities. Counterflow designs are popular in large feed manufacturing plants because they cool evenly with less energy.
Maintenance keeps the pelleting process efficient. Dies and rollers are wear parts and should be replaced every 500-1,000 hours depending on abrasive ingredients like minerals or fishmeal. Regular PDI testing with a tumbling box confirms durability, and screens or hammers in the hammer mill should be checked at the same intervals.
Preventive maintenance also covers the conveyor system, bucket elevator, and screw conveyor, since blockages or worn flights disrupt ingredient batching and dosing. Keeping a spare parts inventory for dies, rollers, and screens reduces downtime and protects throughput capacity.
A practical example: a swine feed mill increased PDI from 85% to 97% by optimizing steam quality and die compression ratio, reducing fines by 30%. That change lowered dust, improved feed conversion ratio, and reduced returns from clogged feeders.
Quality Control and Automation
Quality control in feed production involves sampling at critical points, testing for moisture, protein, and PDI, and using PLC/SCADA systems to automate batching, mixing, and pelleting for consistent output.
Standards such as HACCP, GMP, and ISO 22000 shape how a feed manufacturing plant documents checks, sets corrective actions, and proves that every batch meets specification. Key parameters tracked across the animal feed production line include moisture content, particle size, bulk density, and pellet durability index (PDI).
Automation ties these checks together. A PLC control layer manages ingredient batching, weighing scales, and dosing systems, while SCADA software records trends and flags deviations before finished feed leaves the plant. This combination reduces human error and keeps mash feed, pelleted feed, and extruded feed within target ranges.
Together, QC procedures and automation protect feed safety, support regulatory compliance, and give operators the data needed to adjust the grinding process, mixing process, or pelleting process in real time.
Sampling, Sensors, and PLC/SCADA
Automated sampling systems collect representative samples at intake, after mixing, and after pelleting, while inline sensors monitor moisture (NIR), temperature, and flow rate, feeding data to PLC/SCADA for real-time adjustments.
Sampling frequency usually depends on batch size and risk. Many plants pull a sample every batch at critical control points, while continuous lines may sample hourly. Manual sampling remains common at raw material intake for corn, soybean meal, wheat, and fishmeal, whereas automatic samplers suit high-throughput points after the feed mixer or pelletizer.
Sensor selection matters just as much. Moisture sensors using NIR or capacitance guide dryer and cooler settings. Temperature probes protect the extrusion process and pelleting process from overheating. Flow meters track molasses, fats, and liquid additives, while NIR analyzers estimate protein and fat without waiting on lab results.
On the control side, PLC/SCADA handles recipe management, batching control, trend logging, and alarm management. Recipe management ensures each livestock feed, poultry feed, swine feed, aquaculture feed, or ruminant feed formula is dosed correctly, with weighing scale and dosing system feedback confirming accuracy.
Traceability closes the loop. Batch numbering, RFID tags, and recall management software let a plant trace finished bags back to specific raw materials, premix lots, vitamins, minerals, amino acids, enzymes, probiotics, and additives. If a deviation appears, documented monitoring and corrective actions satisfy HACCP, GMP, and ISO 22000 expectations.
The payoff is measurable. One feed mill reported reducing out-of-spec batches by 40 percent after installing NIR sensors and SCADA integration, largely through faster detection of moisture drift and dosing errors. Similar gains often appear in mixing uniformity, cross-contamination control, and pellet durability index when automation is paired with disciplined sampling.
Packaging, Palletizing, and Logistics
Finished feed is packed into 25 to 50 kg bags or bulk-loaded into trucks at rates up to 1,200 bags per hour, using automated bagging machines, palletizers, and conveyor systems for efficient logistics. The packaging stage is where the animal feed production line meets the customer, so accuracy, speed, and product protection all matter here.
Most feed manufacturing plants offer two delivery formats: bagged and bulk. Bulk delivery suits large livestock and poultry farms that store compound feed in on-site bins. Bagged feed serves smaller farms, retail outlets, and specialty products like aquaculture feed or premix blends.
Bag selection depends on product type and shelf life. Woven polypropylene (PP) bags are durable and moisture-resistant, making them common for pelleted feed. Multi-wall paper bags offer better breathability for mash feed. Laminated or lined bags help protect against humidity when storing extruded feed or crumbled feed.
The packaging line typically includes a bagging machine, a sewing or heat-sealing unit, a checkweigher, and a labeling system. From there, filled bags move by conveyor system to a palletizer, then through a stretch wrapper before entering the warehouse.
Bagging Machine Types Compared
Choosing the right bagging machine affects accuracy, throughput, and operating cost. Four common designs dominate feed mill installations: gross weigh, net weigh, auger, and gravity. Each suits different product characteristics and capacity targets.
| Type | Accuracy | Speed | Best For |
|---|---|---|---|
| Gross Weigh | Moderate | Medium to High | Free-flowing pelleted feed, simple operation |
| Net Weigh | High | High | Premium accuracy, retail bags, varied products |
| Auger | Moderate | Low to Medium | Mash feed, powders, less free-flowing mixes |
| Gravity | Moderate to High | High | Uniform granules, high-volume pelleted feed |
Gross weigh machines fill the bag and weigh the entire unit, which keeps the design simple and affordable. Net weigh systems weigh the product first, then drop it into the bag, delivering better consistency for retail packaging. Auger fillers use a rotating screw to move mash feed and fine blends. Gravity fillers rely on product flow and work best with uniform, free-flowing granules.
Typical costs range from $10,000 to $50,000 for a bagging machine, depending on automation level and throughput capacity. A palletizer usually costs between $30,000 and $150,000, with robotic models at the higher end.
Palletizing, Wrapping, and Labeling
After filling, bags travel by bucket elevator or screw conveyor to the palletizing station. Conventional palletizers stack bags in fixed patterns using mechanical arms. Robotic palletizers offer more flexibility and handle varied bag sizes without mechanical changeover.
Once stacked, pallets pass through a stretch wrapper that secures the load for transport. Labeling systems then apply batch codes, production dates, and nutritional information. Barcode scanning at this stage supports traceability from raw materials through to the final customer.
Traceability matters for feed safety and regulatory compliance. Batch codes on each bag link back to ingredient batching records, mixing process logs, and quality control results. This supports HACCP, GMP, and ISO 22000 requirements during audits or recalls.
Logistics and Outbound Handling
Outbound logistics covers truck loading, rail shipment, and container filling for export. Bulk feed moves through dedicated loading spouts into tanker trucks. Bagged feed loads onto flatbeds or box trucks, often with forklifts moving wrapped pallets directly from storage.
For container filling, workers or automated systems load pallets in patterns that maximize space. Rail transport suits high-volume feed manufacturing plants serving distant regions. Each mode requires coordination between the packaging line, warehouse, and dispatch team.
Automation through PLC control helps synchronize bagging, palletizing, and loading rates. When throughput capacity rises, the packaging line must keep pace with the pelleting process and cooling process upstream. Preventive maintenance on bagging machines, sewing heads, and palletizer grippers reduces downtime and protects output targets.
Safety, Maintenance, and Environmental Compliance
Feed mill safety focuses on dust explosion prevention (NFPA 61), lockout/tagout for maintenance, and environmental compliance with air emission and waste regulations, while preventive maintenance schedules extend equipment life and reduce downtime. In any animal feed production line, these three pillars work together to protect workers, equipment, and the surrounding community.
Dust is the single greatest hazard in a feed manufacturing plant. Grain dust from corn, wheat, and soybean meal can ignite with devastating force when it accumulates in enclosed spaces. An effective aspiration system captures dust at transfer points throughout the grinding process, mixing process, and pelleting process.
Key dust control measures include:
- Aspiration hoods at the hammer mill, feed mixer, and bucket elevator discharge points
- Cyclone separators and bag filters to collect airborne particles
- Explosion venting panels on bins, silos, and enclosed conveyors
- Airlocks to prevent flame propagation between connected equipment
- Regular housekeeping to prevent dust layers exceeding safe thresholds
Beyond dust, maintenance crews must follow lockout/tagout procedures before servicing any feed pellet mill, extruder, or conveyor system. Confined space entry into storage silos requires atmospheric testing, ventilation, and a standby observer. Personal protective equipment, including respirators, hearing protection, and safety glasses, is mandatory near the hammer mill, crumbler, and bagging machine.
Preventive maintenance keeps an animal feed production line running at peak throughput capacity. A structured schedule prevents unexpected breakdowns in the feed pellet mill, extruder, dryer, cooler, and packaging line. Daily checks catch minor issues before they escalate.
A practical maintenance checklist includes:
- Daily: inspect hammers, screens, and belts for wear; check magnet and metal detector function; verify lubrication on screw conveyor and bucket elevator bearings
- Weekly: examine pellet mill dies and rollers for cracking; test airlock seals; clean bag filter elements; calibrate weighing scale and dosing system
- Monthly: replace worn hammers and screens; inspect gearbox oil; test PLC control sensors; review vibration analysis data on high-speed rotating equipment
Maintaining a spare parts inventory of hammers, screens, dies, rollers, belts, and bearings minimizes unplanned stoppages. Predictive maintenance using vibration analysis detects bearing degradation before failure. A preventive maintenance program reduces downtime by 20 to 30 percent, directly improving return on investment.
Environmental compliance covers dust and odor control, waste management, and adherence to regulations from the EPA, OSHA, and local authorities. A feed manufacturing plant must control air emissions from the grinding process, drying process, and cooling process to protect air quality.
Common environmental control measures include:
- Bag filters on aspiration systems to capture fine particulate matter
- Scrubbers to reduce odor from molasses, fishmeal, and meat and bone meal handling
- Recycling of screenings, spilled raw materials, and damaged bags
- Proper disposal of waste oil, used filters, and contaminated packaging
Dust collection systems typically cost between $20,000 and $100,000 depending on capacity and filter type. This investment protects worker health and prevents regulatory penalties. In one case example, a feed mill avoided a $50,000 fine by installing a bag filter system and implementing a dust control program before a scheduled inspection.


